Your Location:Home > Technical Advantages
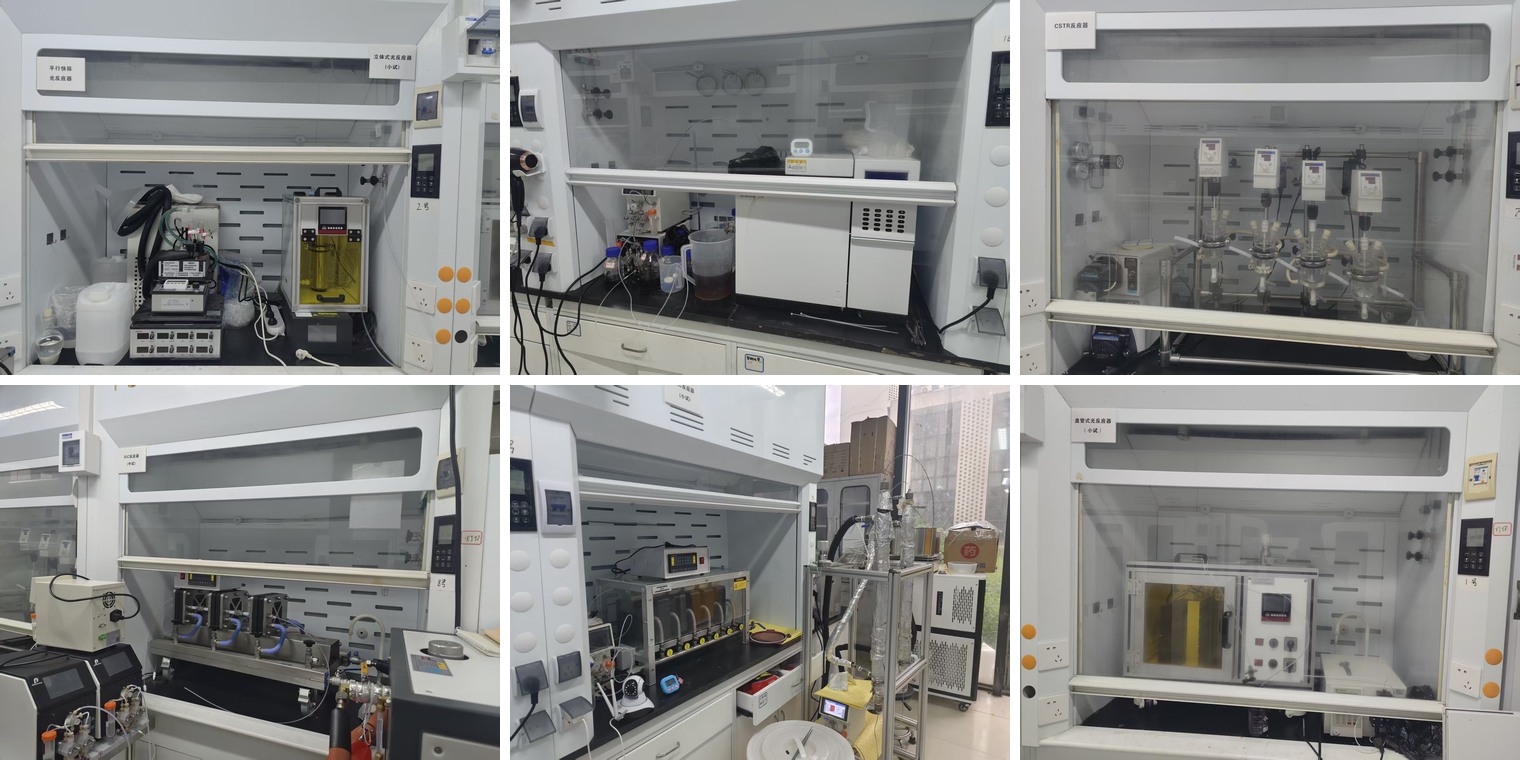
Our product R&D laboratory is located in the High-tech Zone of the Hefei. The modern R&D center covers an area of over 3,000 square meters and is equipped with various professional R&D and analytical instruments including NMR spectrometers, LC-MS systems, liquid chromatographs and gas chromatographs, supporting the full workflow from research, lab-scale trials to pilot production.
Apart from conventional stirred tank reactors, we have established industry-leading specialized reaction platforms to accommodate reaction types difficult to achieve with standard stirring processes, as detailed below.
| Platform | Application Scenarios | Delivered Value |
|---|---|---|
| Continuous Flow / Microreaction Platform | High-pressure Hydrogenation / Photocatalysis / Electrochemistry | Catalysis Platform |
| High-risk, strongly exothermic, gas-liquid multiphase reactions | Functional group transformation, green synthesis | Metal catalysis, enzyme catalysis, asymmetric synthesis |
| Intrinsic safety, precise temperature control, stable processes | Replacement of highly polluting routes, cost reduction and efficiency improvement | Improved selectivity |
Our strong professional technical capabilities ultimately bring customers lower total cost, shorter R&D cycles, higher product quality and better-controlled compliance risks.
Address:Room 1623,Building A, ZhongqiaoCenter,Goverment District,Hefei city,Anhui Province,ChinaEmail:heyuchem@163.com
Tel:15256001178Phone:15256001178